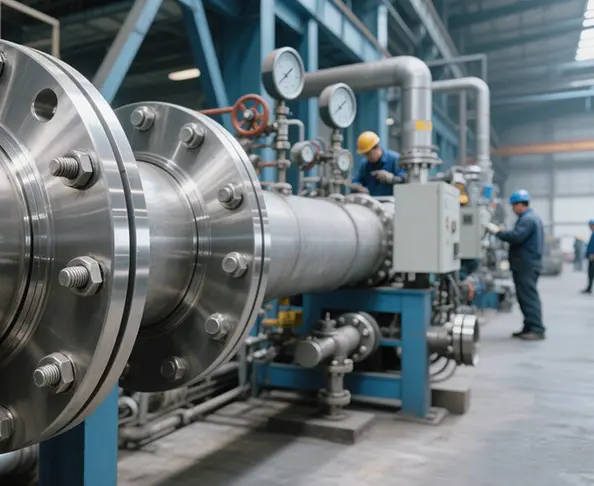
Explore our primary heavy-duty forged flange offerings manufactured to international engineering standards.





A Weld Neck Flange (WN Flange), classified as EN 1092-1 Type 11 or ASME B16.5 Type WN, represents the pinnacle of high-integrity flange engineering. It is distinguished by its long, tapered hub that transitions seamlessly into the nominal wall thickness of the mating pipe.
Unlike flat or slip-on components, weld neck flanges are specifically engineered to transfer stress directly from the flange face to the pipe wall, mitigating high stress concentration at the base of the flange hub. This smooth structural transition is vital under severe operating environments involving extreme hydrostatic pressures, thermal shock, cyclic fatigue loading, and sub-zero bending moments.
When selecting a reliable Weld Neck Flanges Manufacturer & Supplier, EPC contractors and mechanical project managers must evaluate the forging flow lines. Proper closed-die or ring-rolling hot forging aligns the internal steel grain structure parallel to the principal stress axis, delivering superior resistance against fatigue and stress corrosion cracking (SCC).
To assist piping engineering teams in selecting the correct flange specification, the following quantitative engineering matrix contrasts Weld Neck flanges with Slip-On, Socket Weld, and Blind flanges:
| Flange Type | Pressure Class Range | Stress Dissipation Efficiency | NDT / Radiography Compatibility | Typical Pipeline Application |
|---|---|---|---|---|
| Weld Neck (WN) | Class 150 to 2500 / PN6 - PN400 | High (Tapered hub transfers stress) | 100% Full Volumetric Radiography (RT) | High-pressure gas, thermal steam, crude oil export lines |
| Slip-On (SO) | Class 150 to 1500 / PN6 - PN100 | Moderate (Double fillet weld required) | Limited to Surface NDT (PT/MT) | Low-pressure utility lines, municipal water distribution |
| Socket Weld (SW) | Class 150 to 1500 / PN10 - PN100 | Moderate to High (Small bore lines) | Surface NDT (Fillet weld root restriction) | Small-diameter high-pressure chemical instrument tubing |
| Lap Joint (LJ) | Class 150 to 300 / PN10 - PN40 | Low (Relies on Stub End connection) | Visual / Surface NDT on Stub End | Corrosive chemical loops requiring frequent dismantling |
As an established Chinese OEM manufacturer and global supplier, Shanxi Yuxin Casting & Forging Co., Ltd. precision-forges Weld Neck Flanges adhering to all major international standard systems:
ASME B16.5: Covers Pipe Flanges and Flanged Fittings from NPS 1/2" through NPS 24" in Pressure Classes 150, 300, 400, 600, 900, 1500, and 2500.
ASME B16.47 Series A & B: Covers Large Diameter Steel Flanges from NPS 26" through NPS 60". Series A (MSS SP-44) features heavier profiles, while Series B (API 605) provides compact designs for pipeline applications.
EN 1092-1 Type 11: Specifies Steel Weld Neck Flanges across Nominal Pressures from PN 2.5 to PN 400, with nominal sizes ranging from DN 10 to DN 4000.
DIN Standards: Legacy German standards including DIN 2631 (PN6), DIN 2632 (PN10), DIN 2633 (PN16), DIN 2634 (PN25), DIN 2635 (PN40), DIN 2636 (PN64), and DIN 2637 (PN100).
JIS B2220: Japanese Industrial Standards for 5K, 10K, 16K, 20K, and 30K steel pipe flanges.
GOST 12821-80: Russian standard for steel butt-welded flanges operating under pressures from 0.1 to 20.0 MPa (1 to 200 bar).
Material chemistry dictates a flange's mechanical performance under thermal, pressure, and corrosive stresses. We maintain a large inventory of certified raw steel billets across carbon, stainless, alloy, and duplex grades:
| Material Category | Standard Material Grade | Operating Temperature Range | Primary Industrial Application Environment |
|---|---|---|---|
| Carbon Steel | ASTM A105 / Q235B / C22.8 / P250GH | -29°C to +425°C | General oil & gas, high-pressure utility water, steam lines |
| Low-Temp Carbon Steel | ASTM A350 LF2 Class 1 / Class 2 | -46°C to +345°C | Cryogenic gas storage, arctic pipelines, cold climate processing |
| High-Yield Pipeline Steel | ASTM A694 F42, F52, F60, F65, F70 | -29°C to +121°C | High-pressure cross-country transmission oil/gas pipelines |
| Alloy Steel | ASTM A182 F11, F22, F5, F9, F91 | Up to +650°C | Superheated steam, power plant boilers, refinery hydrocrackers |
| Austenitic Stainless Steel | ASTM A182 F304/304L, F316/316L, F321, F347 | -196°C to +815°C | Chemical processing, LNG terminals, marine & offshore systems |
| Duplex & Super Duplex | ASTM A182 F51 (S31803), F53 (S32750), F55 | -50°C to +300°C | Sour oil wells (H2S), subsea manifolds, desalination plants |
Dingxiang County in Shanxi Province, China, is globally recognized by international trade organizations as the official “Hometown of Forging in China.”
The regional industrial cluster consolidates raw steel sourcing from national steel mills, high-efficiency clean energy infrastructure, specialized tooling design, and highly skilled metallurgical workforces within a concentrated 30-kilometer radius. This unique industrial density enables Shanxi Yuxin Casting & Forging Co., Ltd. to offer unmatched lead times, structural quality control, and direct-from-factory pricing advantages to global distributors and engineering firms.
By eliminating intermediate trading markups and operating dedicated ring-rolling and die-forging production lines, Yuxin provides a 15% to 30% total-cost-of-ownership (TCO) advantage on international project orders without compromising technical parameters or certification rigor.
Established in 1992 in the Zhuangli Enclave Industrial Zone, Shanxi Yuxin Casting & Forging Co., Ltd. has developed into a fully integrated manufacturer of carbon, stainless, and alloy steel forged components.
In deepwater platforms and subsea Christmas tree piping, flanges must resist massive hydrostatic pressures and corrosive seawater. Yuxin supplies Class 1500 and 2500 Weld Neck RTJ flanges forged from Duplex F51 or Inconel 625 cladding, meeting strict NACE MR0175 sour service standards.
High-temperature refinery loops operate continuously above 500°C under thermal cycling. Our ASTM A182 F11 and F22 Chrome-Moly weld neck flanges undergo precision thermal heat treatment (Normalizing + Tempering) to prevent creep deformation over decades of uninterrupted service.
Main steam piping in power generation facilities requires 100% full-volumetric non-destructive testing. Weld neck flanges manufactured by Yuxin feature strict bore tolerances to match high-pressure steam pipes, eliminating flow restrictions and turbulence-induced erosion.
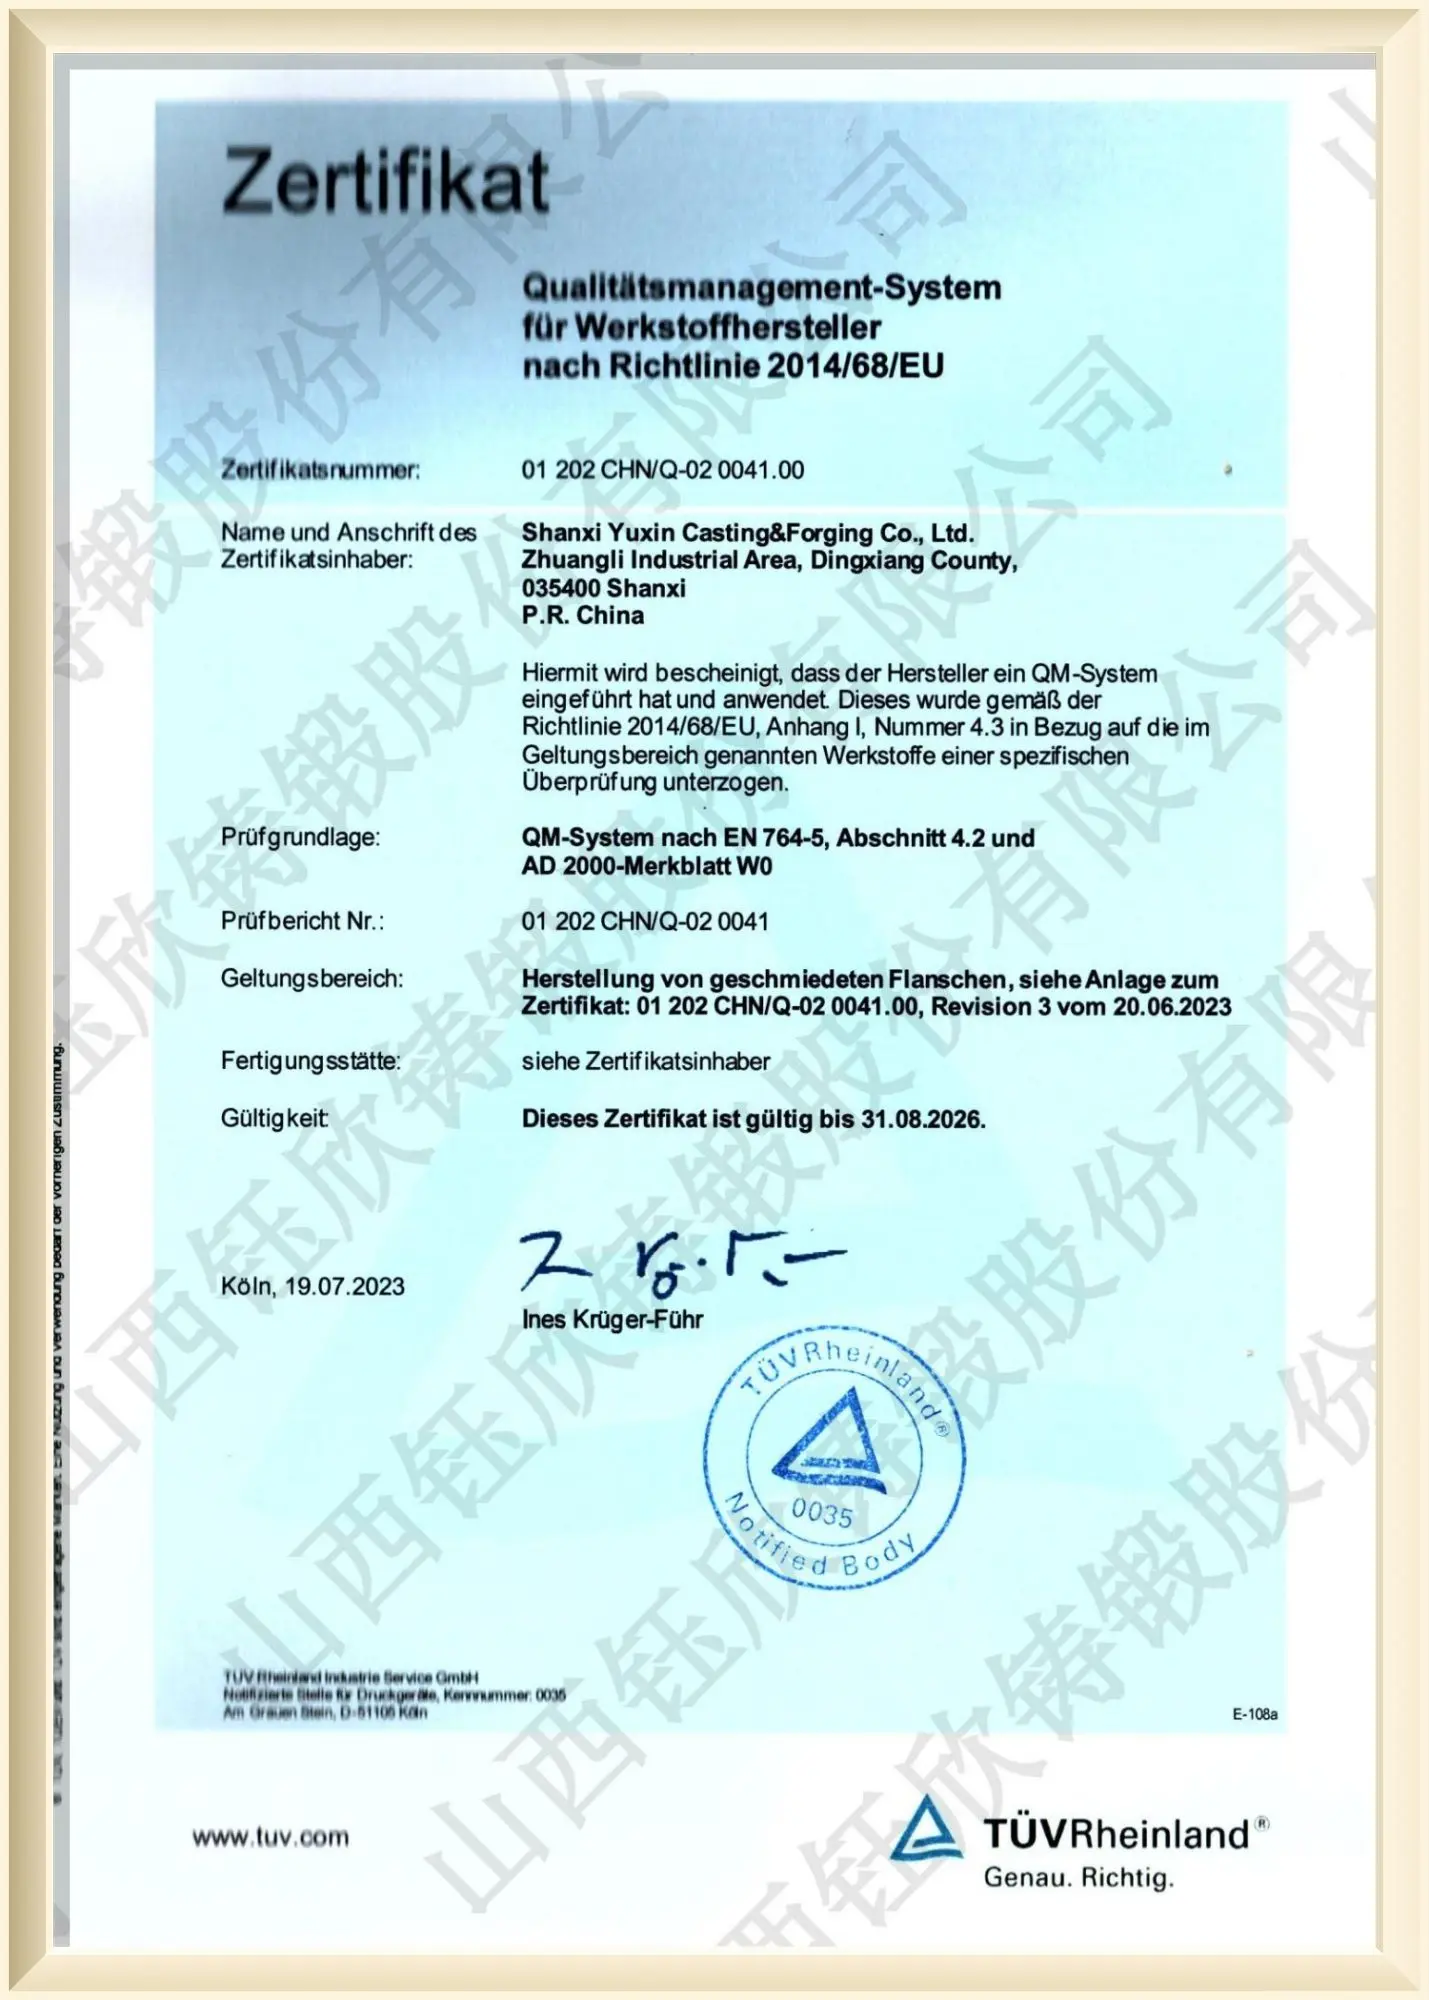
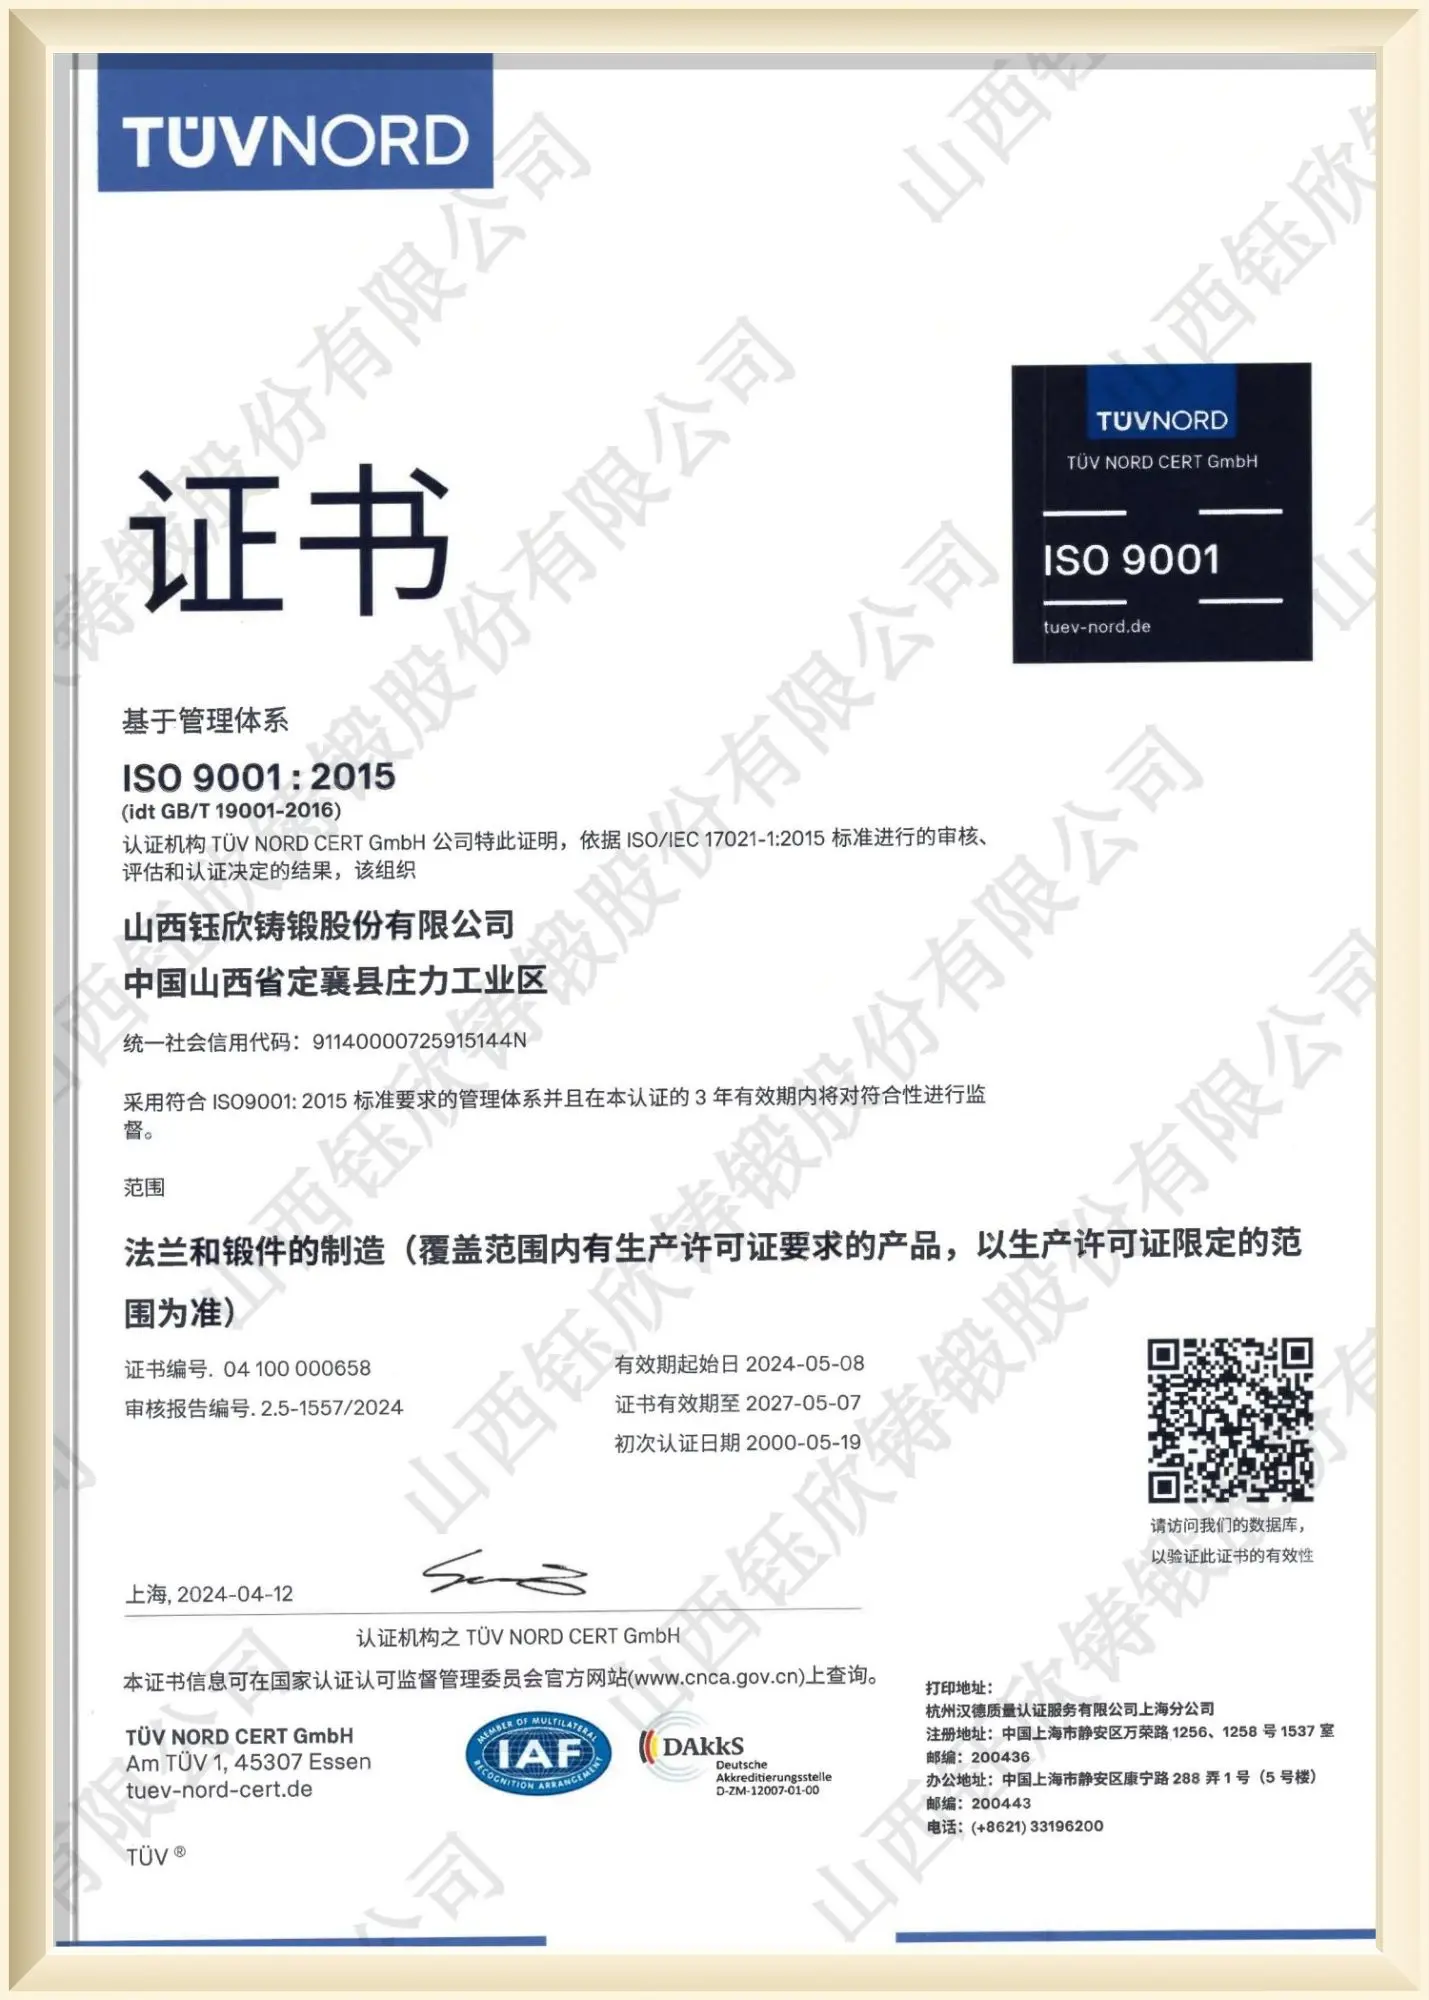
In critical pressure equipment manufacturing, structural reliability is non-negotiable. Shanxi Yuxin enforces a rigorous Quality Management System audited by international classification bodies.
Every critical export batch undergoes non-destructive evaluation performed by qualified Level II / III inspectors according to ASNT and EN standards:
We provide comprehensive inspection documentation packages with every shipment, ensuring seamless engineering audits:
Modern CNC radial-axial ring rolling machines ensure uniform forging ratios across large-diameter flanges up to 3,000mm. This eliminates structural porosity and drastically improves dimensional precision, reducing post-forge machining waste.
As the global energy transition accelerates, clean hydrogen transport pipelines demand ultra-low permeability forgings. Yuxin works with low-sulfur vacuum-degassed steel heats to prevent hydrogen embrittlement in high-pressure gas lines.
By transitioning forge reheating furnaces from coal to natural gas and electric induction heating systems, Yuxin has reduced carbon intensity per ton of finished flange output by over 35% since 2020.
From raw steel billet inspection to final export crating, complete traceability is maintained under one roof.
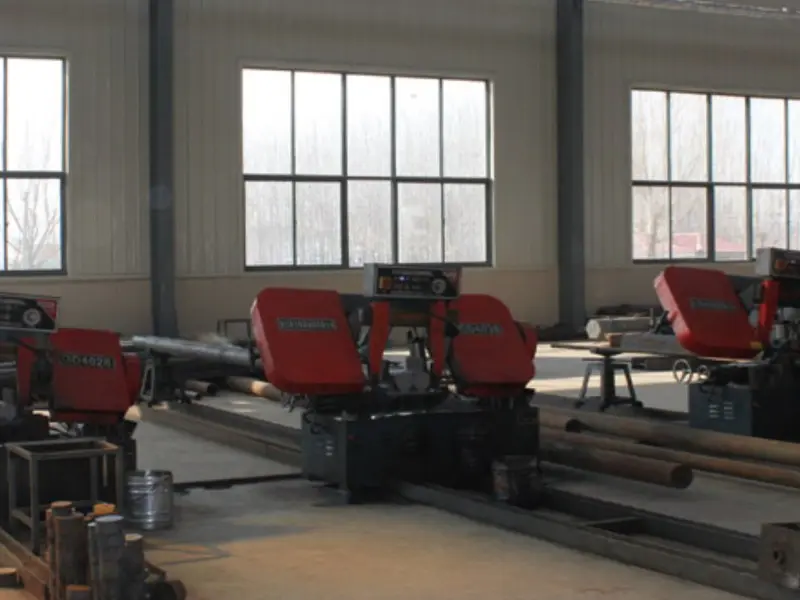
Verified prime steel billets undergo spectroscopic heat chemical analysis before saw cutting.
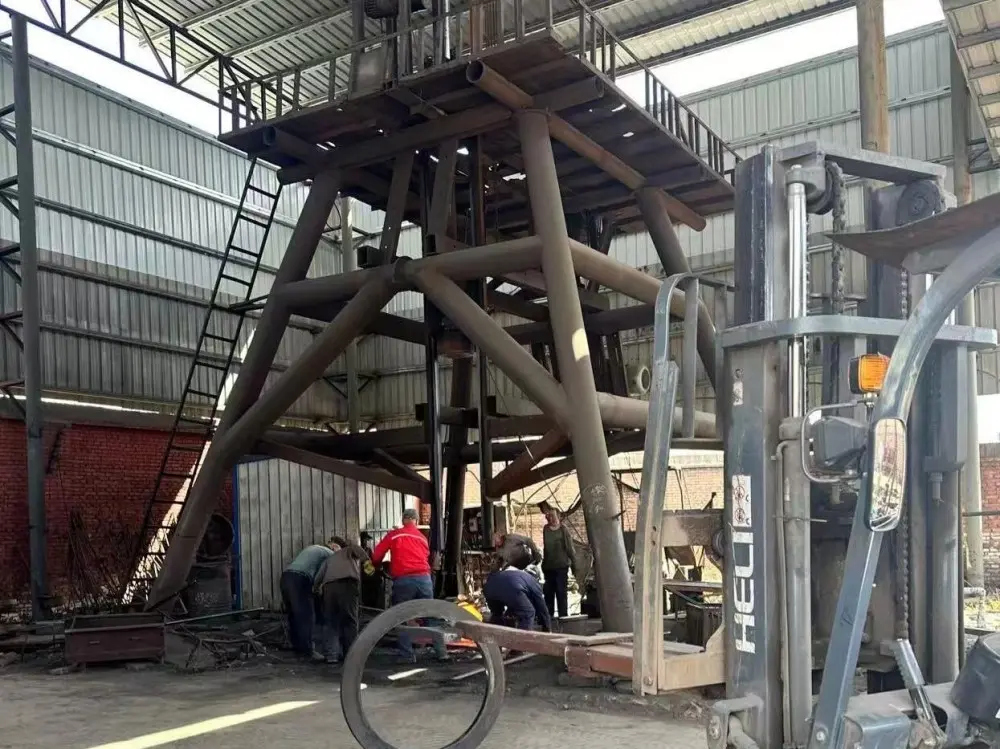
Billets are heated to 1,200°C and forged under hydraulic hammers to refine internal grain structure.
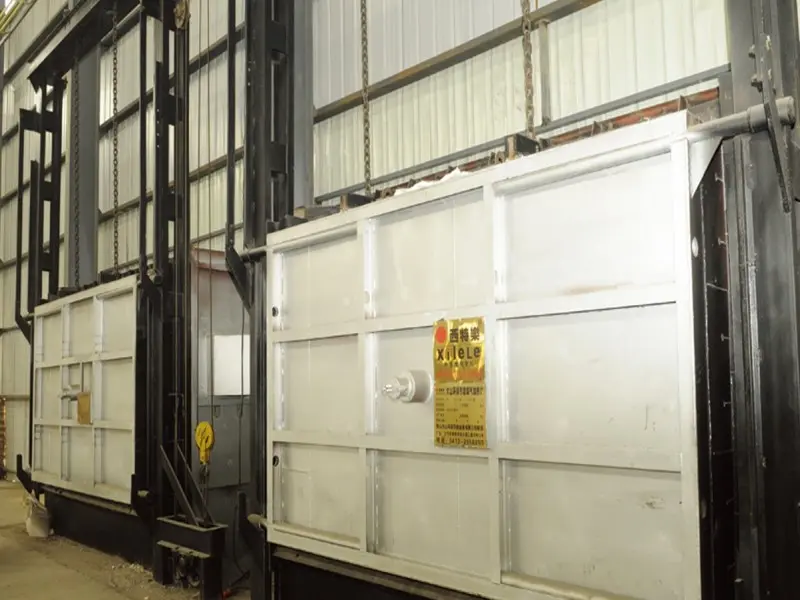
Normalizing, tempering, or solution annealing to achieve target mechanical strength and ductility.
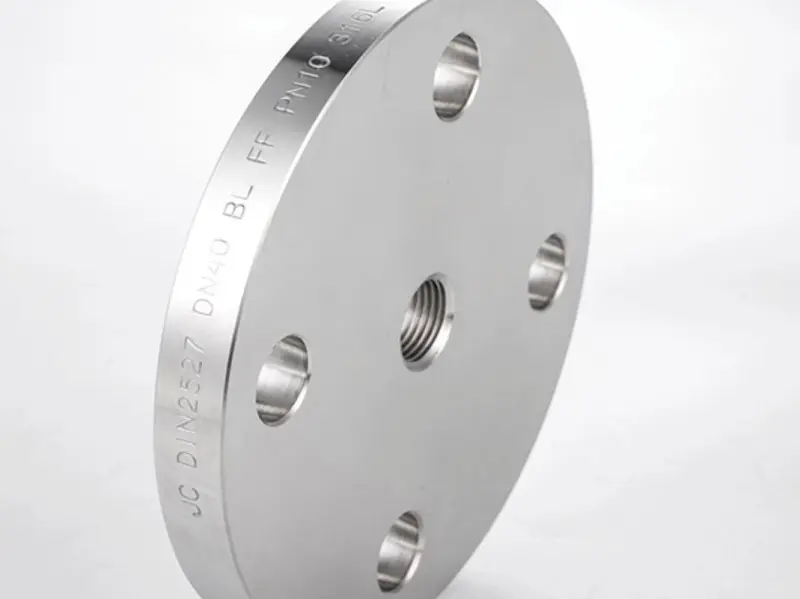
Permanent low-stress die stamping of heat number, nominal size, pressure rating, and material grade.
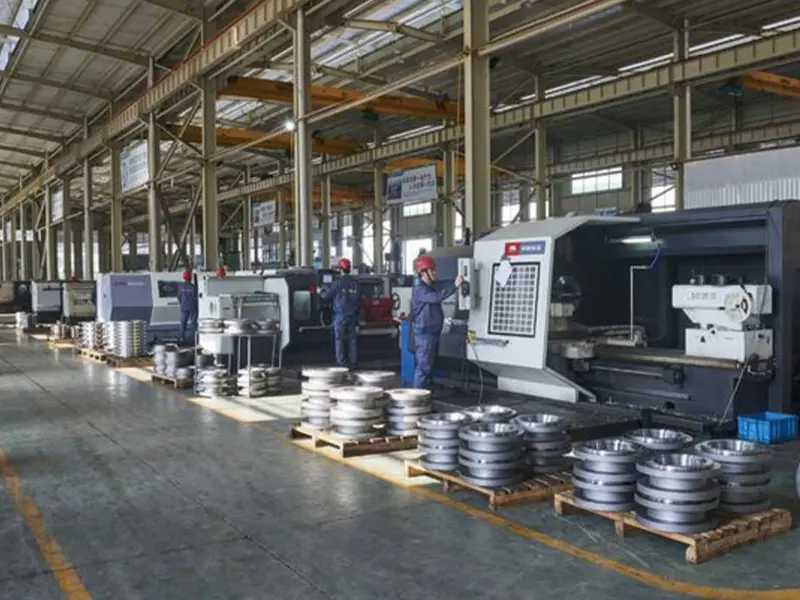
High-precision vertical lathes turn the flange profile, tapered hub, bore ID, and raised sealing faces.
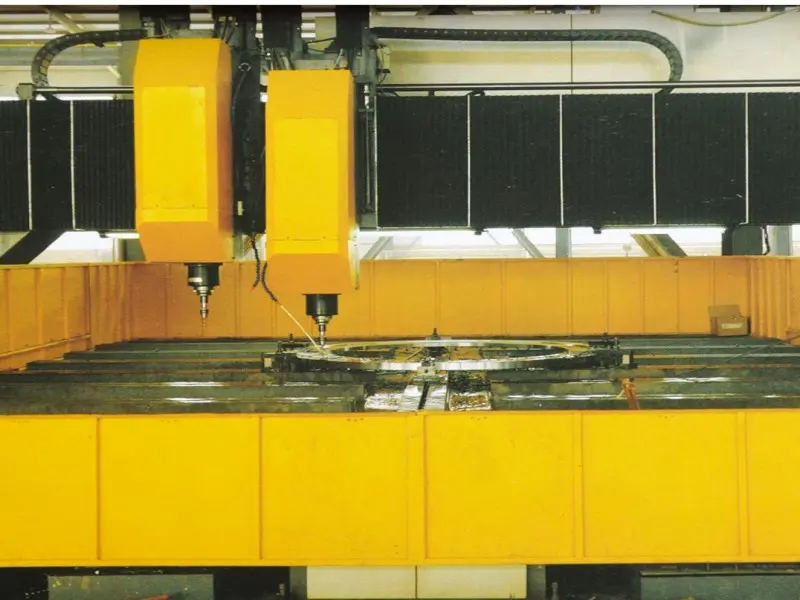
Automated multi-spindle CNC drilling guarantees exact bolt circle diameter (BCD) alignment.
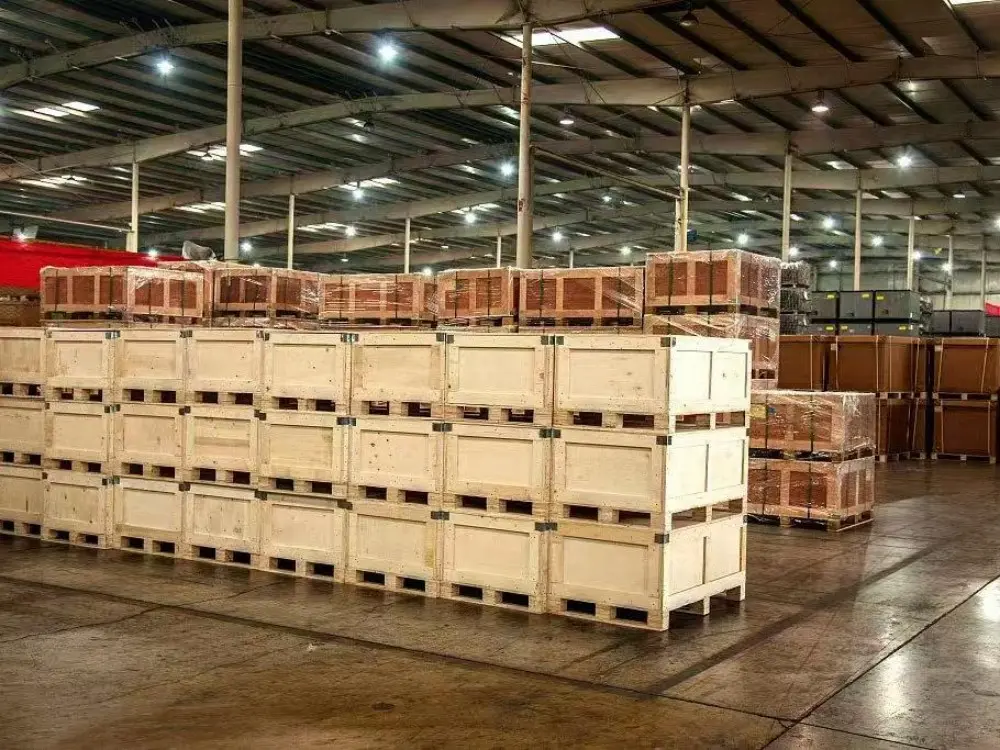
Anti-rust oil/varnish application, plastic cap end protection, and seaworthy plywood case packing.
Third-party witness inspections and live video factory audits welcomed anytime.
Schedule VisitExplore custom plain, slip-on, reducer, and ring flange configurations ready for global dispatch.


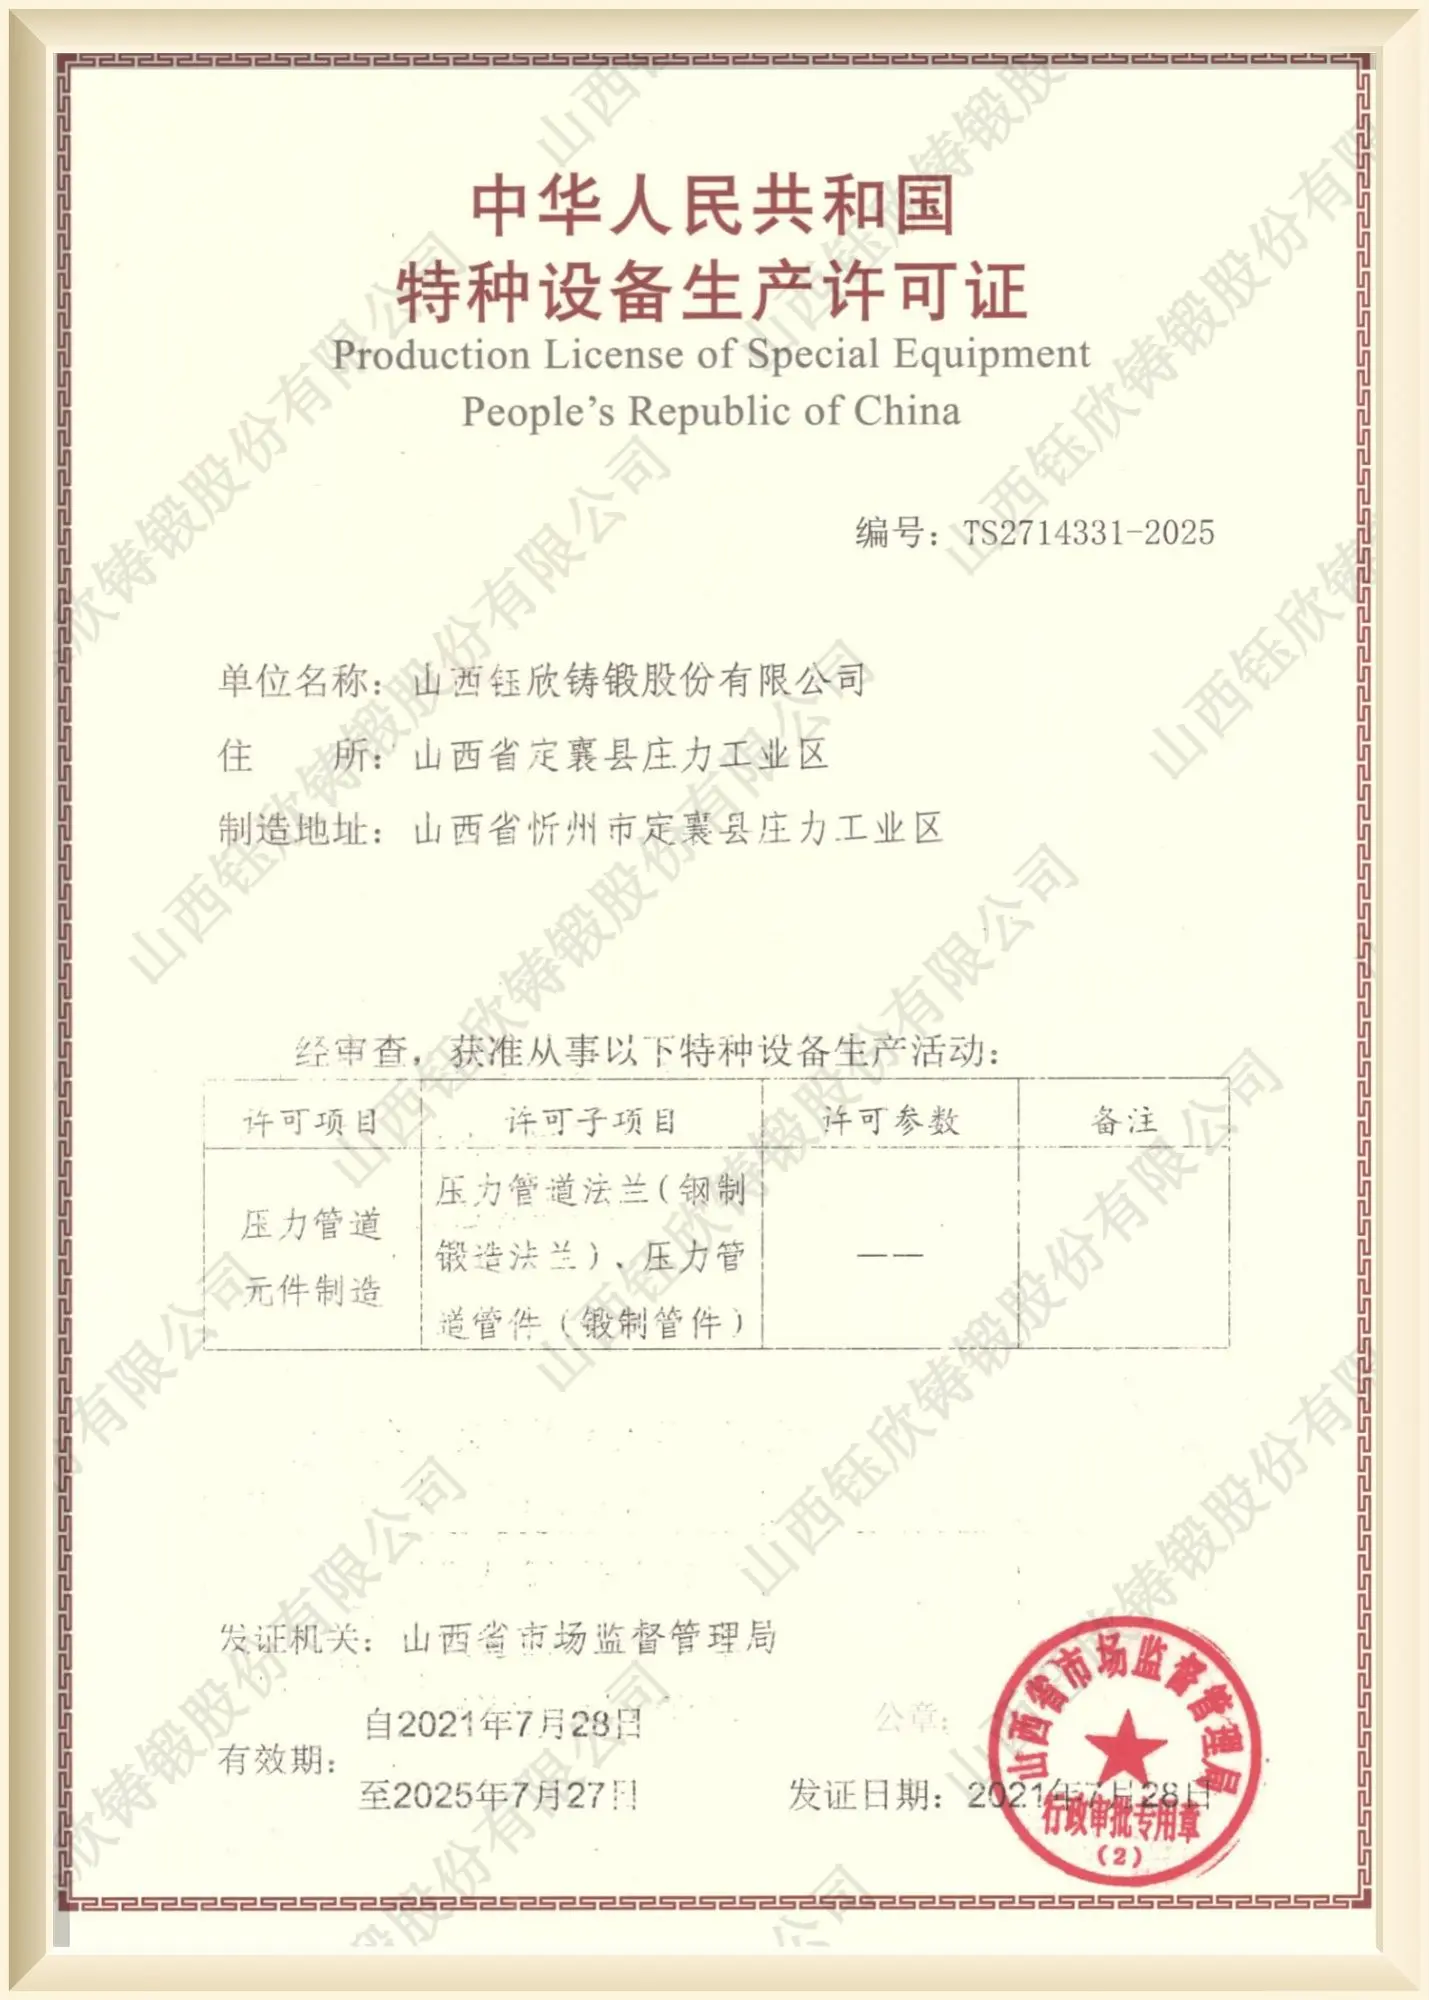
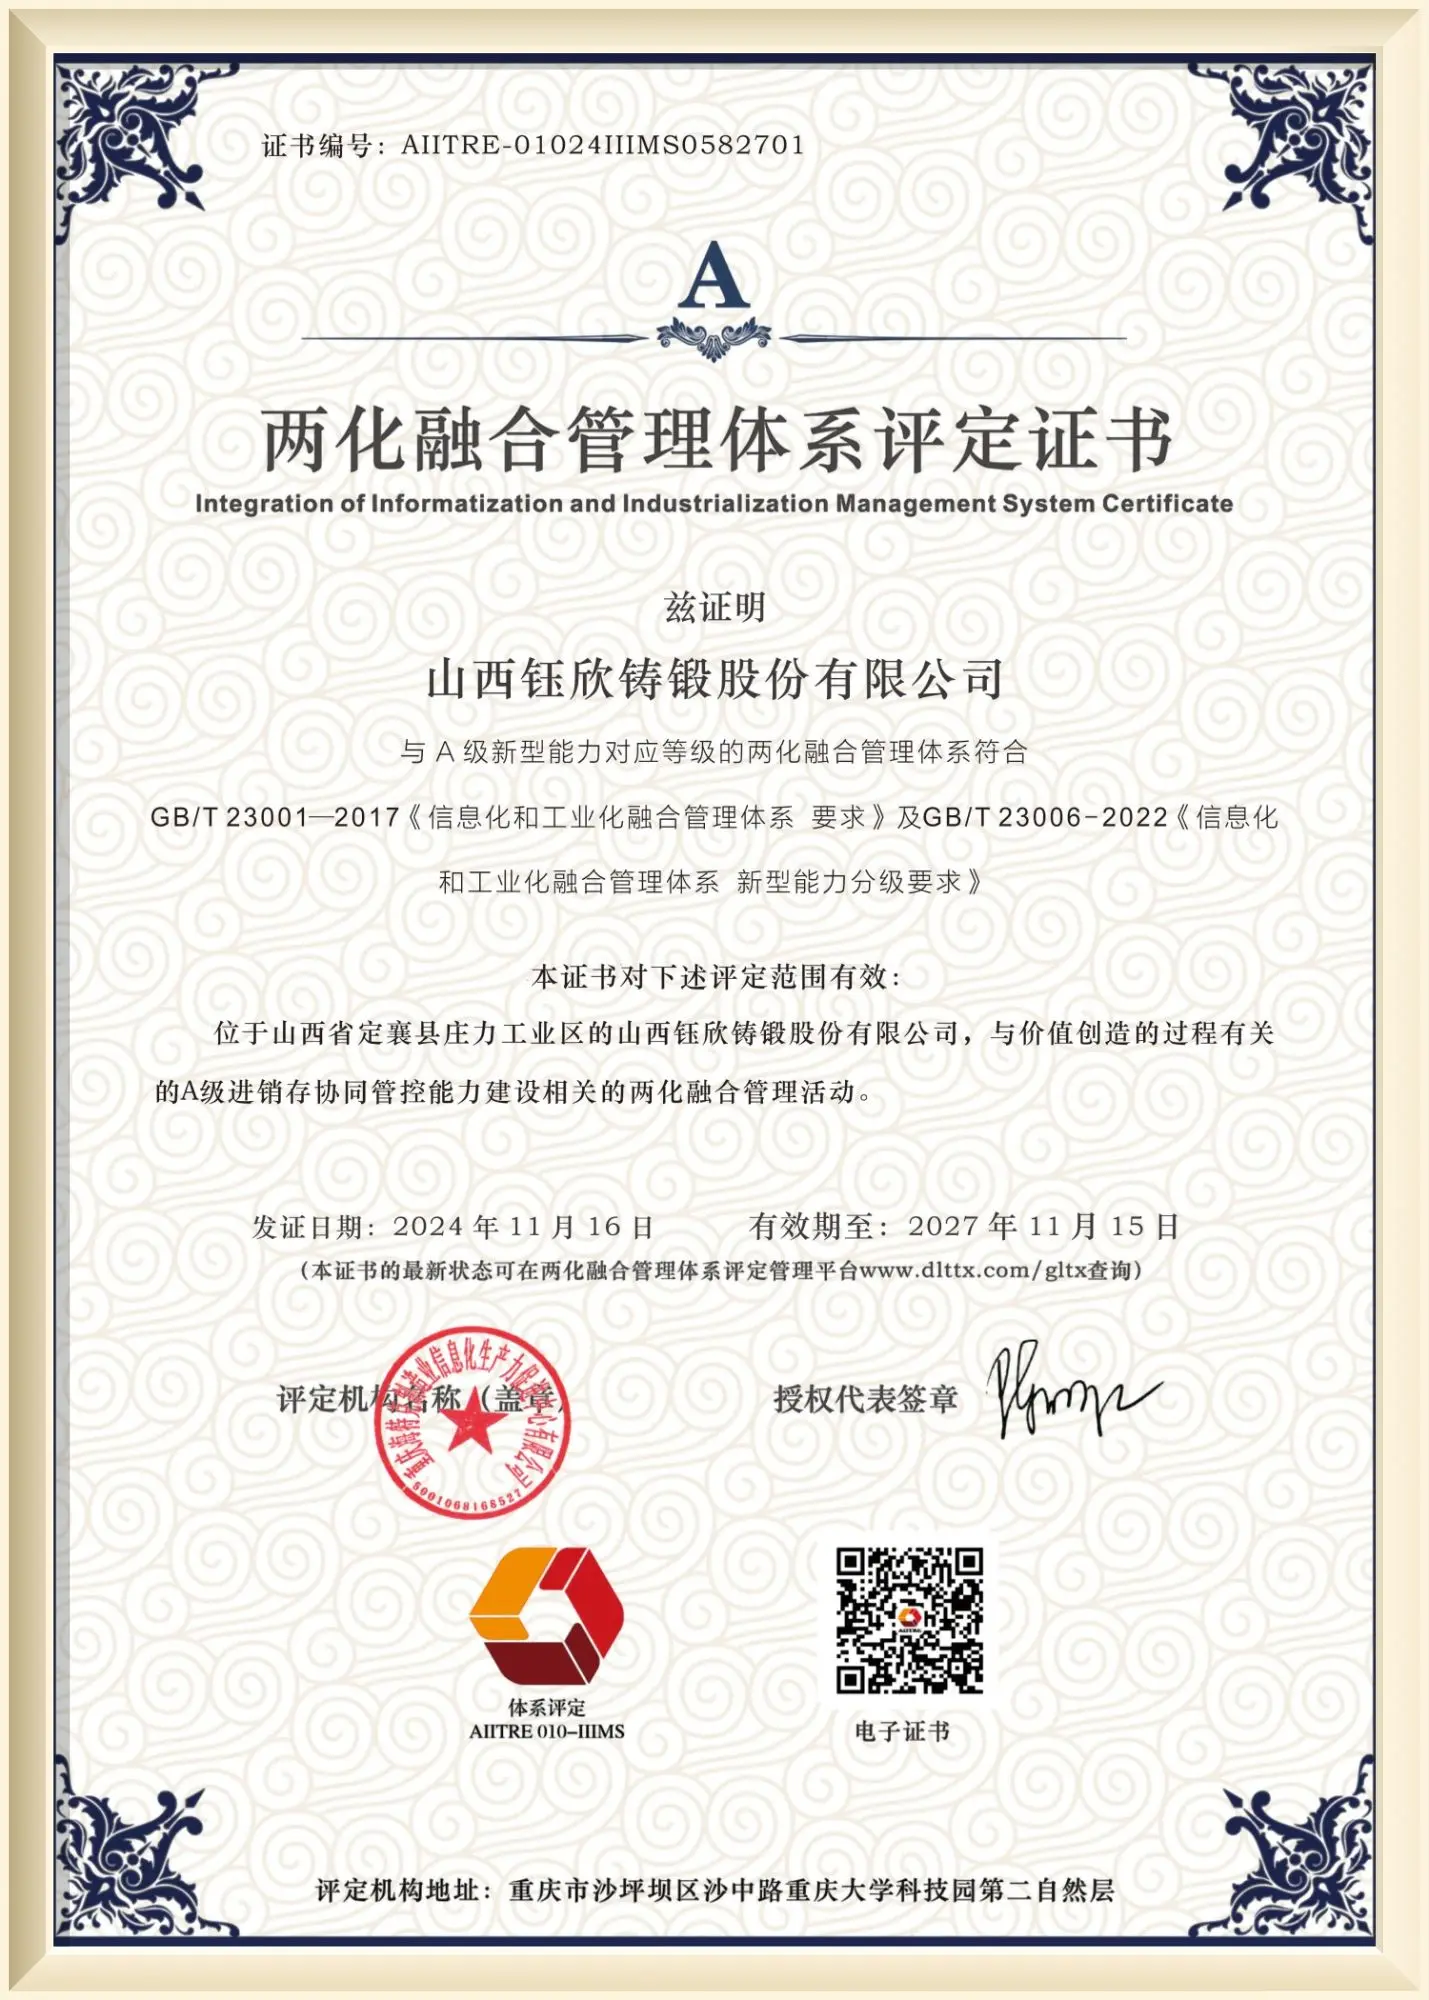
Tested and certified by major international inspection authorities for world-class pipeline safety.


Detailed answers to technical, quality, and commercial inquiries addressed daily by our engineering sales desk.
Weld Neck Flanges feature a tapered hub that transfers mechanical stress directly into the connected pipe wall, minimizing localized stress concentration at the base of the flange. Furthermore, WN flanges are joined via a 100% full-penetration butt weld, allowing 100% volumetric radiography (RT) inspection. Slip-On flanges rely on double fillet welds which create stress risers and cannot undergo full volumetric radiographic testing, restricting their use in high-pressure or cyclic thermal environments.
When ordering Weld Neck Flanges, you must specify the pipe Schedule (e.g., Sch 40, Sch 80, Sch 160, XXS) or exact internal diameter (ID). Unlike Slip-On flanges where the bore is oversized to slide over the pipe, a Weld Neck flange bore is machined to match the pipe's internal wall precisely. Matching the bore prevents internal fluid turbulence, pressure drops, and erosion at the weld root joint.
Every shipment includes a EN 10204 3.1 Mill Test Certificate (MTC) detailing raw material heat number, chemical composition, tensile/yield strength, elongation, hardness, Charpy V-notch impact values, heat treatment records, and non-destructive examination (UT/MT/PT) reports. EN 10204 3.2 certificates issued by third-party agencies (SGS, TÜV, BV) are available upon project request.
Standard carbon steel sizes (A105, PN16/Class 150) held as ready-for-machining forged blanks ship within 7 to 15 days. Custom forged-to-order alloy or duplex steel flanges generally require 20 to 35 days depending on raw heat availability and heat treatment cycles. We support flexible MOQs for project trial orders and distributor stock replenishment.
Yes. Our engineering team routinely produces non-standard flanges, heavy wall hubs, tube sheets, and forged rings up to 3,000mm outer diameter. We work directly from customer CAD (DWG, STEP, PDF) files, engineering custom forging dies in-house to reduce tooling lead time.
Flange faces and bevels are thoroughly cleaned, coated with rust-preventive yellow varnish, black rust-inhibiting paint, or transparent oil, and fitted with heavy-duty plastic end protectors. Shipments are packed inside fumigation-free wooden crates or securely steel-strapped onto solid export pallets lined with moisture barrier film.
Submit your flange schedule, material specifications, or custom drawings. Our engineering team provides itemized technical and commercial quotes within 24 hours.
Connect directly with our export engineering department for project inquiries, technical specifications, and factory audit scheduling: